We bend tube in house on a Transfluid DB 2076 mandrel bender, at our workshop in Little Hulton, Manchester. Stainless steel, mild steel and aluminium, up to 76 mm diameter.
Most fabricators send tube bending out. We brought it in, because on handrails, balustrades and tube frames the quality of the bend is the quality of the finished job, and because waiting a week for a bending house to fit you in is a poor reason for a project to slip.
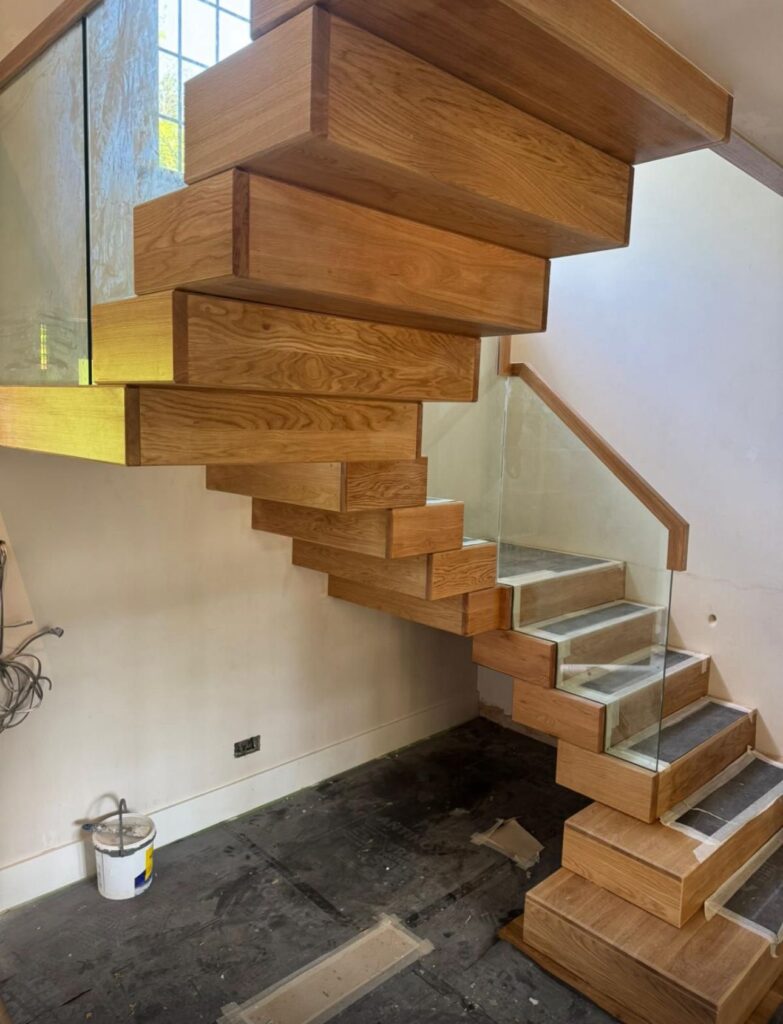
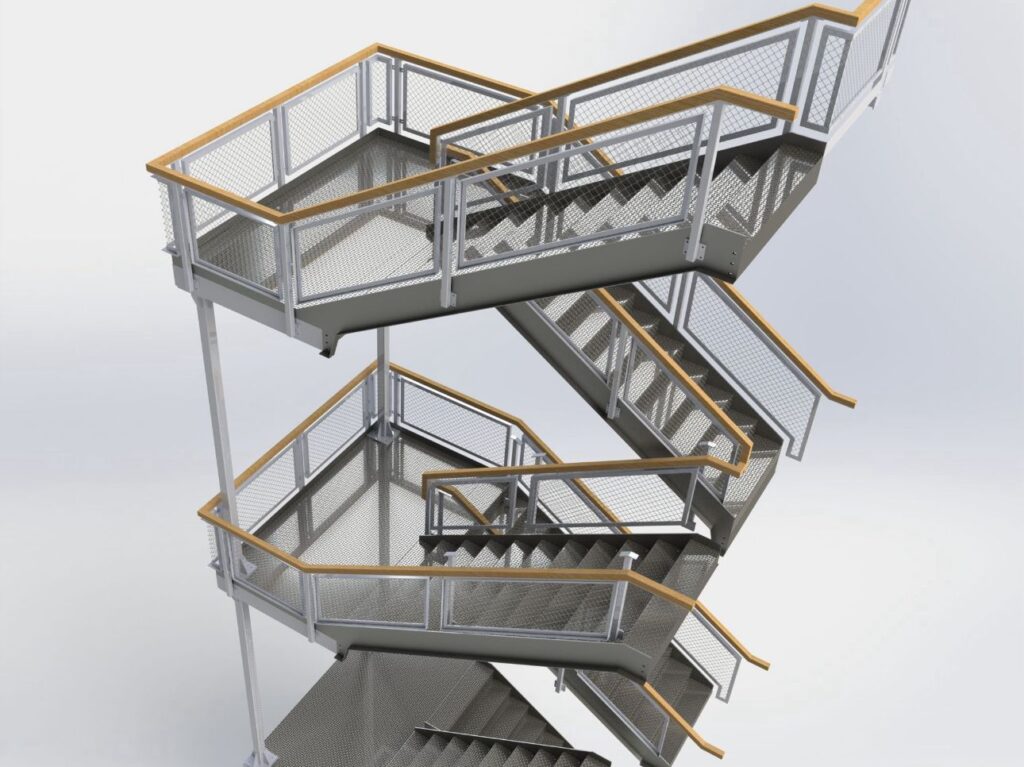
When you bend a tube, the outside wall stretches and the inside wall compresses. Without support, the section deforms: the outside thins, the inside wrinkles, and the round profile goes oval or kinks outright.
A mandrel is a former that sits inside the tube and travels with the bend, holding the wall in shape as it goes round. The result is a bend that keeps its round section and its wall thickness, with no wrinkling on the inside radius and no flattening on the outside.
On a polished stainless handrail this is the difference between a run that reads as one continuous line and one that visibly changes shape at every corner.
Wrinkles cannot be polished out. They have to be ground back, which thins the wall and usually looks worse.
That 76 mm is the machine's capacity. What is achievable on any given job depends on the tooling and the wall thickness of your tube, so send us the specification and we will confirm before you commit to a design.
If you are a fabricator, shopfitter or installer without a mandrel bender, we will bend for you. Send tube and a drawing, or let us supply the material as well. We are used to working to someone else's specification.
We do not approach your client.
76 mm diameter is the machine capacity. Achievable radii depend on the tooling and the wall thickness, so confirm the specification with us first.
Yes. That is a large part of why the work stays in house. We bend, weld, dress and polish under one roof, so the finish is controlled throughout.
Press or roll bending gives no internal support, so thin-wall tube tends to flatten or wrinkle. Mandrel bending supports the wall from inside and holds the round section. For visible handrail work the difference is obvious.
Usually. Send a sample or a measured drawing and we will tell you honestly whether we can match it.
Yes, and batches. Both are normal work.
Send a drawing, a sketch or a photograph with the tube diameter and wall thickness to info@ironworxengineering.co.uk, or call 01925 747465.
WhatsApp us